Capability · In-house
In-house tool and die design for custom extrusions.
We design and make the extrusion dies for your parts in our own tool and die room in Oceanside, California. Our engineers can help with the design before the die is made.
Why the die decides the part
Every extrusion takes its cross-section from a die. Resin goes into the hopper, a turning screw conveys it, and friction and added heat melt it. A metal die then shapes the melt into your cross-section, and the part is cooled as one continuous length. Change the opening in the die and you change the part.
That is why our dies are made in-house. Extrusion dies are made by our own tool and die makers to your specifications, and die development is in-house too. When a part carries a co-extruded stripe or a second material, those join at the die, so the same tool and die room supports our co-extrusion work.
The dies we make shape the custom profiles, tubing, pipe and rods we extrude for you, up to 3 in across. You can see the tool and die room in our factory tour.
Tool and die room
What our tool and die room covers.
From your drawing to a finished die in one plant. Open items are marked; everything else is published and verified.
| Topic | What we publish |
|---|---|
| Die design | Our engineers can help with the design before the die is made. |
| Die making | Our own tool and die makers, in our in-house tool and die room in Oceanside, CA.Ref. 8, source |
| Die development | In-house (die R&D).Ref. 8, source |
| Cross-sections | Profiles up to 3 in wide, tubing 1/16–3 in outside diameter, pipe 1/8–3 in; every product within 3 in.Ref. 2, source |
| Co-extrusion | Co-extruded stripes and second materials join at the die (co-extrusion). |
| Drawing files | STEP, STP, IGES, IGS, DWG, DXF, STL, IronCAD, SolidWorks, PDF, ZIP, JPG or PNG, up to 50 MB each.Ref. 7, source |
| Die lead time | Ask for it with your quote. |
Examples
Dies, and the parts they shape.
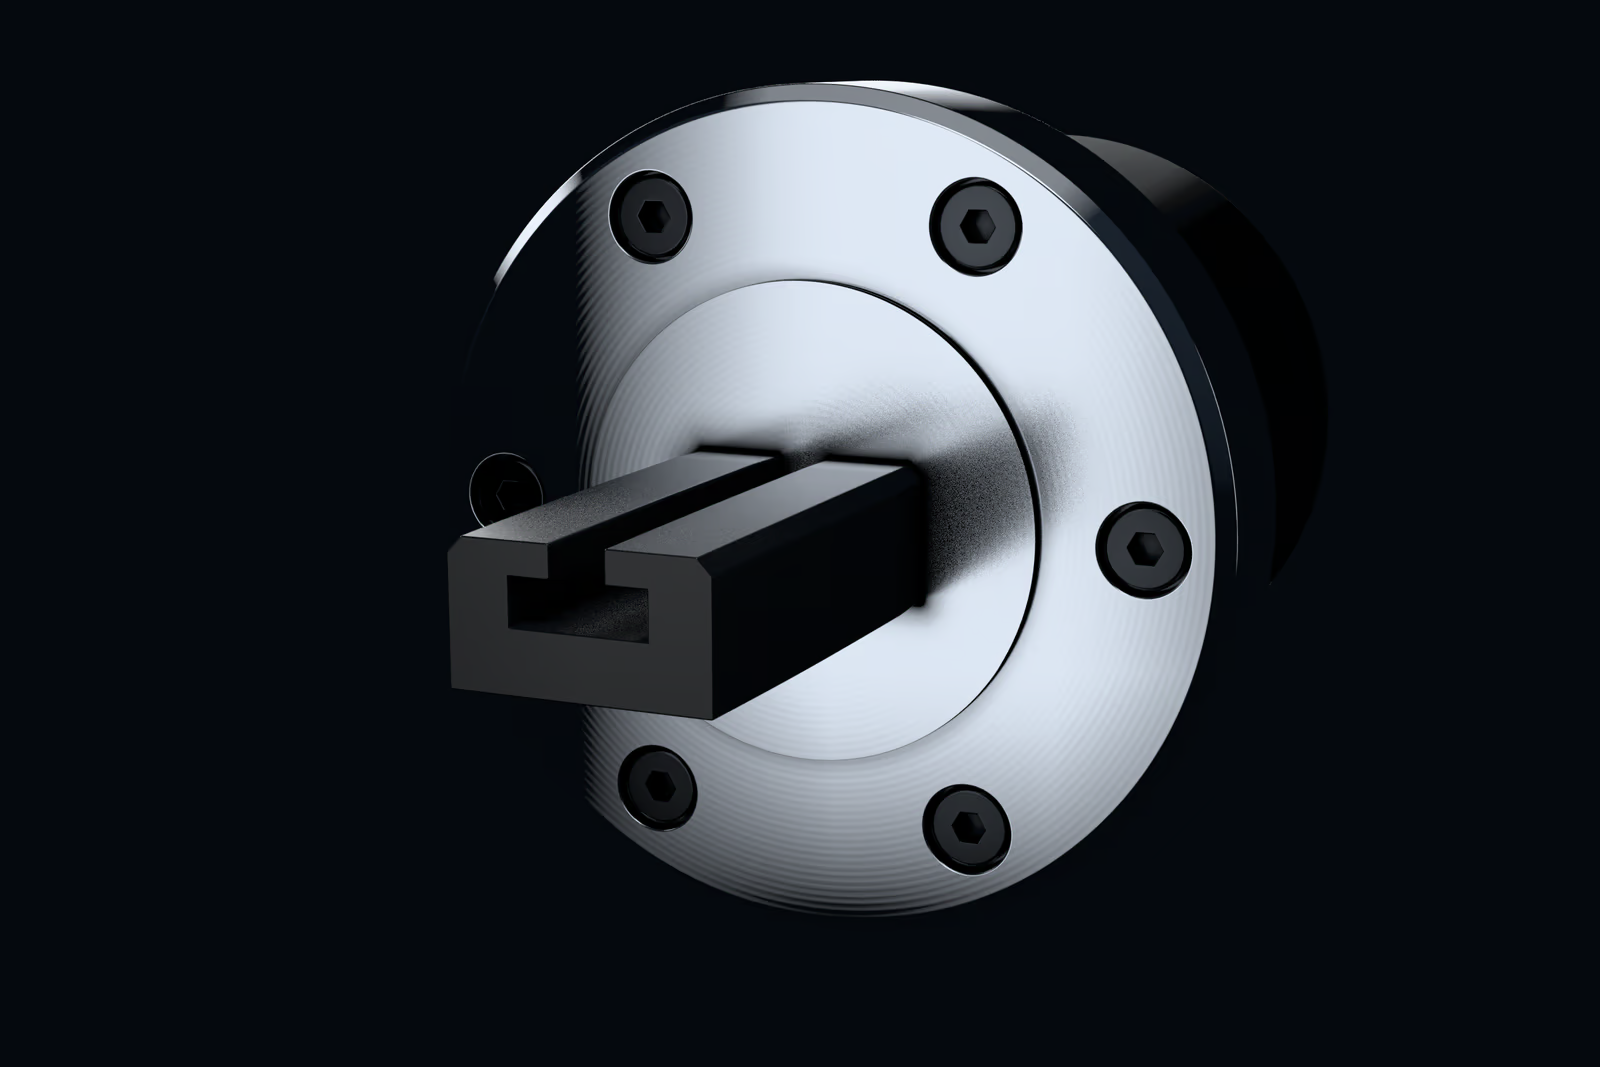
FIG. 01 A generic T-slot track die, with a cut length of profile in its opening to show the section. Calpex dies are made in our in-house tool and die room. 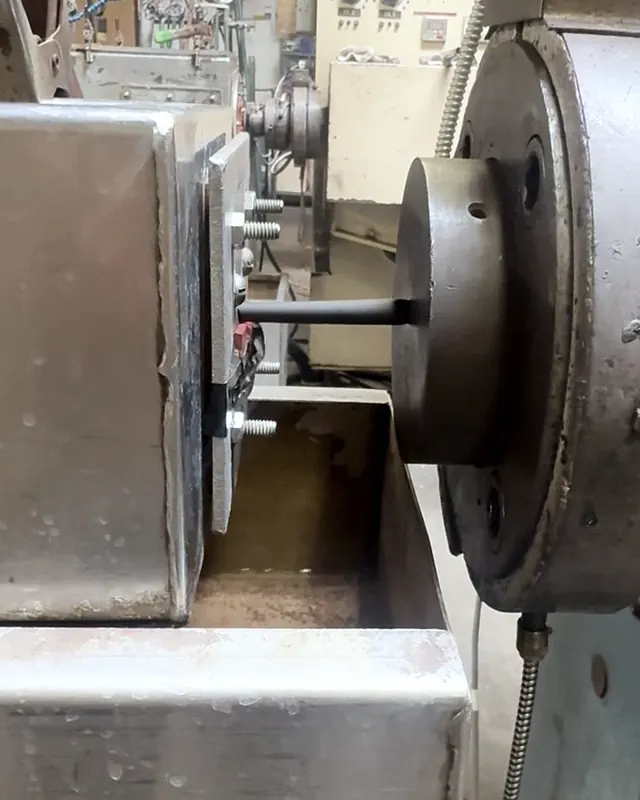
FIG. 02 A die on one of our lines in Oceanside, with the part running into the cooling trough (still frame). 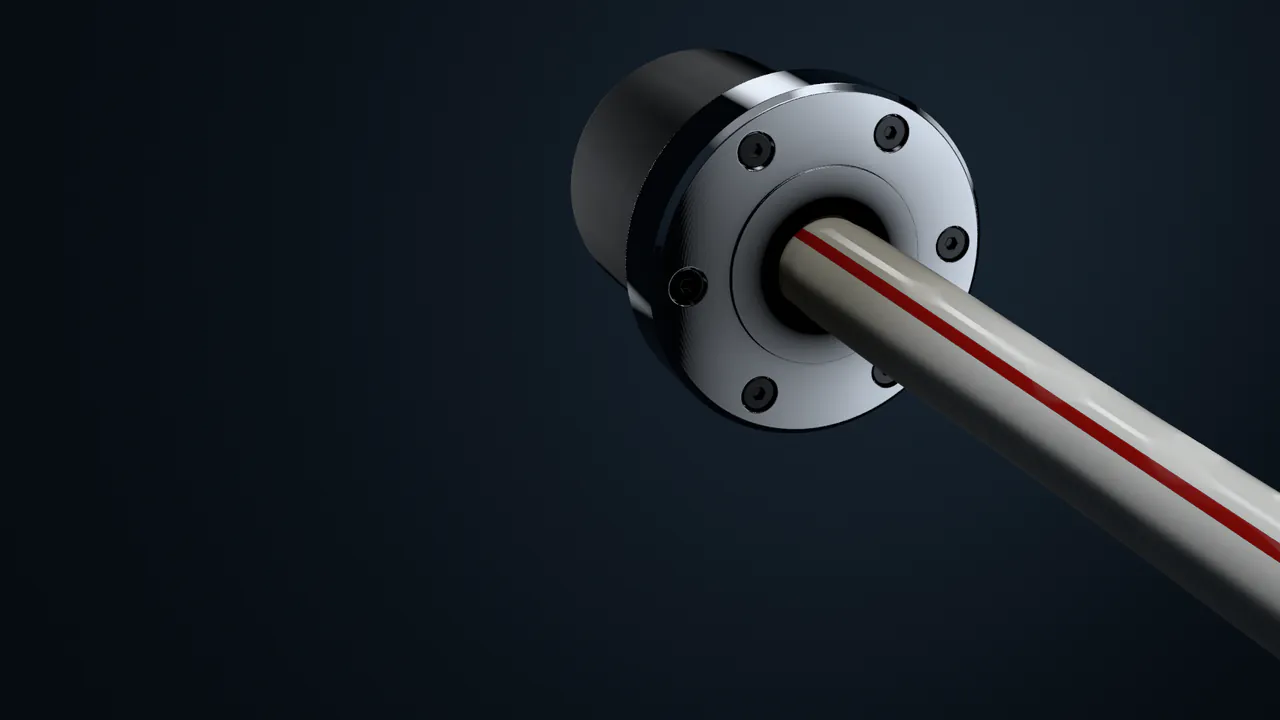
FIG. 03 A striped tube leaving a generic die face. 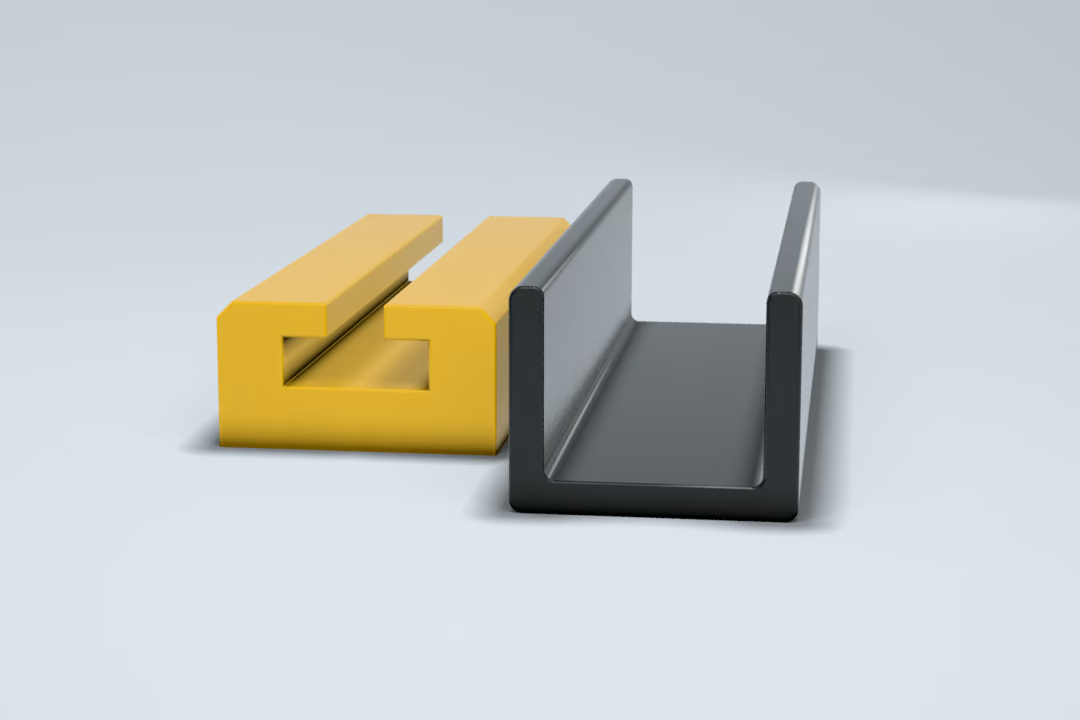
FIG. 04 Profiles: each cross-section comes from its own die. 
FIG. 05 Tubing winding onto a reel at the end of one of our lines in Oceanside (still frame).
Limits
Limits, and what comes with your quote.
- 3 in is the maximum. Every die we make is for a product within the 3 in cap.
- No published die lead time. Ask for it with your quote.
- No published tolerances. Tolerances depend on material and geometry, and we quote them from your drawing.
FAQ
Tool and die questions.
Do you make your own extrusion dies?
Yes. Extrusion dies are made by our own tool and die makers in our in-house tool and die room in Oceanside, California. Die development is in-house too.
Can your engineers help before the die is made?
Yes. Our engineers can help with the design before the die is made. Attach your drawing to a quote request to start.
Can one die run two materials?
Yes. In co-extrusion, co-extruded stripes and second materials join at the die, so two or more materials leave it as one part.
How long does a new die take?
Die lead time depends on the part, so ask for it with your quote request. A whole order typically takes 4–6 weeks with shipping, quoted per project.
Which drawing files can I send?
Attach your drawing to the RFQ form. It takes common CAD and drawing formats, including STEP (STP), IGES (IGS), DWG, DXF and STL as well as PDF and JPG, and lists every accepted type; 50 MB per file is allowed.
Next step
Send the print. We’ll make the die and the part.
Attach your drawing to a quote request, or call us.
Request a quote Call (760) 254-9162
- ISO 9001:2015
- Since 1980
- Made in Oceanside, CA